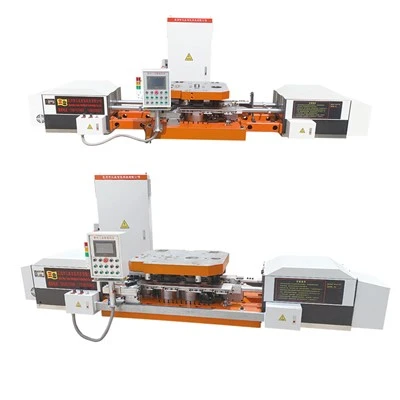
If you’ve ever walked the floor of a bearing manufacturing plant, you’ve seen a Bearing Ring Former (BRF) working overtime, punching and shaping raw steel into the precise, smooth rings that make up the core of everything from car wheels to industrial gearboxes. As someone who’s spent 12 years selling BRFs and supporting operations across North America, Europe, and Southeast Asia, one question comes up in every factory walkthrough and sales call: “How often should I replace the mold on my BRF?” Bearing Ring Former
I get it—mold replacement isn’t cheap. Every downtime window you schedule to swap out molds costs production, and a mold changed too early is wasted money. Change it too late, and you’re looking at scrap rings, quality rejects, and even damaged BRF components. It’s a balance, and there’s no one-size-fits-all answer—until you dig into the factors that actually drive mold wear. Let’s break this down, based on what I’ve seen from hundreds of clients, and the industry data that backs it up.
First, let’s get one thing straight: mold life isn’t measured in calendar months. It’s measured in hits. A “hit” is one full cycle of the BRF: feeding raw bar stock, forming the ring blank, ejecting the part. For standard carbon steel bearing rings (the most common type), a well-built, properly maintained mold will usually last between 200,000 to 500,000 hits. That number jumps to 700,000+ hits for stainless steel, which is softer and less abrasive, but drops to as low as 80,000 hits for high-alloy steel used in heavy-duty industrial bearings. That range is a starting point, but it’s just that—a starting point.
Why such a big gap? Let’s talk about the first variable: material hardness and type. Mold wear is fundamentally abrasive and adhesive. When you’re forming metal, the hard grains in the raw bar stock scrape against the mold surface, wearing it down slowly over time. If that raw stock is a high-alloy tool steel with a Rockwell hardness of 55 HRC, it’s like sandpaper against your mold—hardened H13 tool steel mold material, the standard for BRF molds, wears faster here than it would against mild carbon steel at 30 HRC.
Adhesive wear is another big one. When hot, formed metal sticks to the mold surface, leaving tiny particles that build up and create rough spots. Those spots then catch on the next ring blank, causing minor deformities, scrap, and more wear over time. Clients that run their BRFs without proper lubrication or controlled forming temperatures see adhesive wear 2–3 times faster than those that follow recommended process parameters.
Then there’s operating conditions. I worked with a plant in Detroit last year that ran its BRF 24 hours a day, 6 days a week, forming 100mm bore wheel bearing rings for light trucks. They were changing their molds every 120,000 hits, and they had a 18% scrap rate on rings with uneven wall thickness and surface finish defects. We sent a field service rep to audit their process, and he found two big issues: they were using a generic lubricant instead of a specially formulated metalforming oil for BRF operations, and their forming temperature was running 50°F too high. After we adjusted those settings, they extended mold life to 275,000 hits, and their scrap rate dropped to 4%. That’s the kind of quick win we see all the time—your operating environment is just as important as the mold itself.
So, what about maintenance? A lot of clients think a mold is a set-it-and-forget-it part, but that’s the farthest thing from the truth. Proper mold care can double or even triple its lifespan, and neglect can cut it in half. Let’s be specific here: after every 20,000 hits, you should perform a “light touch-up” where you clean the mold with a media blast (using fine glass beads, not abrasive sand) to remove built-up debris, inspect for minor scratches, and reapply a thin layer of anti-wear coating. Every 100,000 hits, that’s when you do a full inspection: measure the mold’s dimensional tolerances (most BRF molds have a required tolerance of ±0.0005 inches for ring diameter), repair any small chips with precision welding and grinding, and recoat the working surface.
I had a client in Poland who skipped these touch-up steps. They’d run their molds until they started seeing rejects, then do a full rebuild. Their mold life was 220,000 hits. Once we put a scheduled maintenance plan in place—light touches every 20k, full inspections every 100k, and replacing the mold’s core working inserts (the part that actually contacts the raw steel) every 150k hits—they extended total mold life to 400,000 hits, and reduced their mold-related maintenance costs by 35%. That’s the kind of payoff that makes the small up-front maintenance well worth it.
Now, let’s talk about the warning signs that tell you it’s time to replace your mold, regardless of hit count. You don’t have to wait until you hit that 200,000 mark to pull a mold. Here’s what to watch for:
First, dimensional defects. If your rings are consistently coming out 0.002 inches smaller or larger than your required diameter, or have uneven wall thickness across the entire ring, that’s a clear sign the mold surface is worn. Minor size shifts can sometimes be adjusted with machine parameters, but if it’s happening every cycle, the mold is done.
Second, surface finish issues. Bearing rings need a smooth, defect-free surface to handle the high loads they’ll see in operation. If you start seeing micro-scratches, pitting, or discoloration on your rings, that’s either built-up debris on the mold or worn surfaces that are catching the metal. Either way, it’s a sign the mold is reaching end of life.
Third, scrap rate spikes. I always tell clients to track their scrap by cause. If 70% of your rejects are coming from form-related issues (not from raw material or machining errors), that’s mold-related wear. A sudden jump in scrap from less than 3% to over 10% is almost always a mold problem, even if you’re still well under your projected hit count.
Finally, machine performance issues. If your BRF is making unusual noises during the forming cycle, or the ejection mechanism is struggling to push rings out, that’s often because a worn mold is creating more friction between the ring and the tooling, putting extra strain on the machine. If you start seeing signs of BRF wear like broken punches or bent cylinders early, that’s usually a result of running a mold past its life.
Now, let’s address some common myths I’ve heard over the years. The first is: “A new mold is always better.” That’s true, but a well-maintained mold that’s only a few thousand hits from its full life will produce just as good a part as a brand new one. I’ve had clients hold onto perfectly good molds for 10,000 extra hits because they scheduled production runs around their maintenance windows, instead of rushing to buy a new mold.
Second myth: “Harder mold material lasts longer.” Not always. H13 tool steel is the standard because it balances hardness, toughness, and wear resistance. A mold made with a ultra-high-hardness tool steel might wear faster because it’s more brittle, leading to chipping and cracking at lower hit counts. We’ve tested molds with different coatings too: titanium nitride (TiN) coatings last about 15% longer than uncoated molds, and diamond-like carbon (DLC) coatings can add up to 40% to life for low-abrasion applications. The right coating, paired with the right base material, matters more than just picking the hardest material you can find.
Another question I get a lot: “Can I repair a mold instead of replacing it?” The answer is yes, up to a point. The core working insert of a BRF mold—the part that makes contact with the raw bar stock during forming—is the only part that actually wears out. The outer frame and structural components of the mold almost never need to be replaced. So, if your mold’s insert is worn or chipped, you can send it in for precision grinding, welding of minor defects, and recoating, which costs about 30–40% of the price of a new mold. I recommend this for inserts that have less than 50% of their working surface worn. If the insert is more than 70% worn, repair isn’t cost-effective anymore, and you should replace it.
So, putting this all together, what’s a practical guideline for BRF mold replacement? Here’s what I advise clients, regardless of their operation:
- Start with a baseline: For standard carbon steel bearing rings, track hits per mold. Use 300,000 hits as your initial target, adjust up or down based on your material and operating conditions.
- Implement a scheduled maintenance plan: Light touch-ups every 20,000 hits, full inspections every 100,000 hits, repair inserts every 150,000 hits.
- Watch for warning signs: Dimensional defects, surface finish issues, scrap rate spikes, and increased machine strain—these can mean replacement is needed before you hit your projected hit count.
- Evaluate repair vs. replacement: If your mold’s working insert is less than 70% worn, repair is a cost-effective option. If it’s beyond that, new is better.
Now, let’s talk about how this aligns with our experience as BRF suppliers. We design every mold to handle maximum loads, and we provide clients with custom maintenance checklists tailored to their specific BRF model and production line. We’ve also found that clients who work with us to set up a predictive maintenance plan for their molds see a 25% reduction in mold replacement costs, a 10% drop in scrap rates, and less downtime from unexpected machine issues.
I’ll be honest: there’s no perfect number for “how often” to replace a BRF mold. Every operation is different, every part is different, and every maintenance routine is different. But the worst thing you can do is either guess at replacement intervals or wait until you have a pile of scrap rings to figure out something’s wrong.

If you’re currently running BRFs and struggling to balance mold replacement costs, scrap rates, and downtime, that’s what we do. We’ve worked with operations ranging from small job shops with one BRF to large OEMs with 20+ lines, and we can audit your process, track your wear, and help you set a maintenance schedule that works for your bottom line. Whether you need to replace a worn mold, repair an existing one, or invest in a new BRF line, we’re here to help you get the most out of your tooling and your production.
Nut Former References
- ASM International. (2019). Tool Materials for Metal Forming. Volume 14: Forming and Forging, 2nd ed.
- Bearing Manufacturers Association. (2021). Best Practices for Precision Ring Forming Operations. Technical Report BMA-2021-004.
- Groover, M. P. (2020). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems. 7th ed. Wiley.
- International Organization for Standardization. (2018). ISO 10303-242: Industrial automation systems and integration — Product data representation and exchange — Part 242: Application protocol: Process manufacturing.
Quanzhou Sanye Intelligent Technology Co., Ltd.
As one of the most professional bearing ring former manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy customized bearing ring former made in China here from our factory. Welcome to contact us for quotation.
Address: Anhai Town, Jinjiang City, Fujian Province, China
E-mail: jack_tmm@163.com
WebSite: https://www.qzsymanipulator.com/
